From Stock Mould to Something Entirely Yours
Decoration, colour matching and private mould development, all handled in-house.
Each method suits a different surface, budget and print detail. We will tell you which one fits your artwork before you commit.
Silkscreen Printing
Ink applied directly to the component. Best for solid colours and simple logos. Cost-effective from 1,000 pieces, and durable against oils and alcohol.
Hot Stamping
Metallic foil pressed under heat. Delivers a genuine metallic finish that printing cannot match. Gold, silver, rose gold and holographic available.
Spray Coating
Full-body colour in matte, gloss or soft-touch. Turns a clear or white component into any Pantone. Adds a premium tactile quality.
Labelling
Pressure-sensitive or shrink-sleeve labels. The most flexible option for multi-SKU lines and short runs, with full-colour photographic detail.
In-Mould Labelling
Label fused into the component during moulding. Cannot peel or scuff, and keeps the pack mono-material for recycling.
Embossing & Debossing
Raised or recessed detail moulded into the surface. No ink, no foil, no wear. Works best on larger logos and pattern work.
Private mould development
When no existing format fits, we design and tool one. You own the mould, and the shape stays exclusive to your brand.
Typical timeline is 10–14 weeks from approved drawing to first production run. Tooling cost depends on complexity and cavity count; we quote it up front, with no staged surprises.
Discuss a Private Mould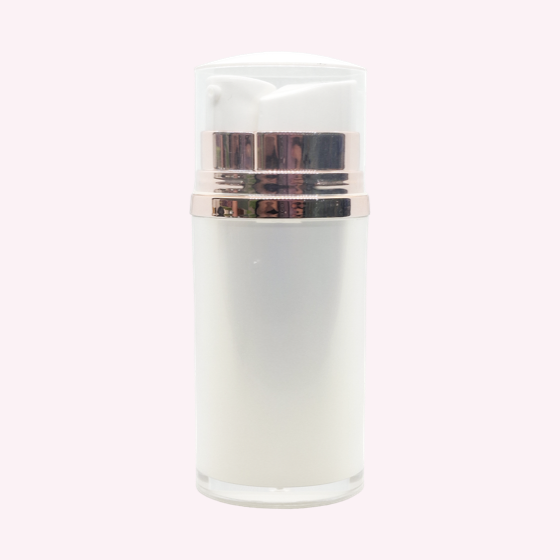
Week 1: Brief
We review your concept, volume and budget, then confirm whether a stock mould will work or tooling is genuinely needed.
Week 2–3: Design
2D drawings and 3D renders for approval. We flag wall thickness, draft angles and anything that will cause moulding defects.
Week 4: Prototype
3D-printed prototype so you can hold the shape and test ergonomics before committing to steel.
Week 5–12: Tooling
Mould manufacture and trial shots. You receive T1 samples for functional and compatibility testing.
Week 13: Approval
Final samples with decoration applied. Nothing enters production until you sign off a physical pack.
Week 14+: Production
Full run with in-process quality control. Repeat orders from an existing mould run in 3–4 weeks.
PET: clarity and barrier
Excellent clarity, good chemical resistance and widely recycled. Our default for bottles where the customer should see the product. Not suitable for hot fill above 60°C.
PP: closures and flexible parts
Tougher and more heat-resistant than PET. Standard for caps, closures and tubes. Accepts soft-touch coating well.
HDPE: opaque and light-blocking
Naturally opaque, protecting light-sensitive formulas. Common for supplement bottles and lotion packs.
Acrylic: weight and depth
Thick-wall clarity that reads as glass at a fraction of the weight. Usually paired with an inner PP bottle for airless systems.
Glass: premium and inert
Completely inert, so no interaction with any formula. Heavier shipping cost, but unmatched perceived value and infinitely recyclable.
Aluminium: light and recyclable
Very light for its strength and accepted by virtually every recycling programme. Ideal for tins, pomade jars and solid formats.
Not sure which route fits?
Send us your product details and target price. We will tell you honestly whether stock, customisation or a private mould makes most sense.